Color consistency on different materials: fabric, metal, plastic
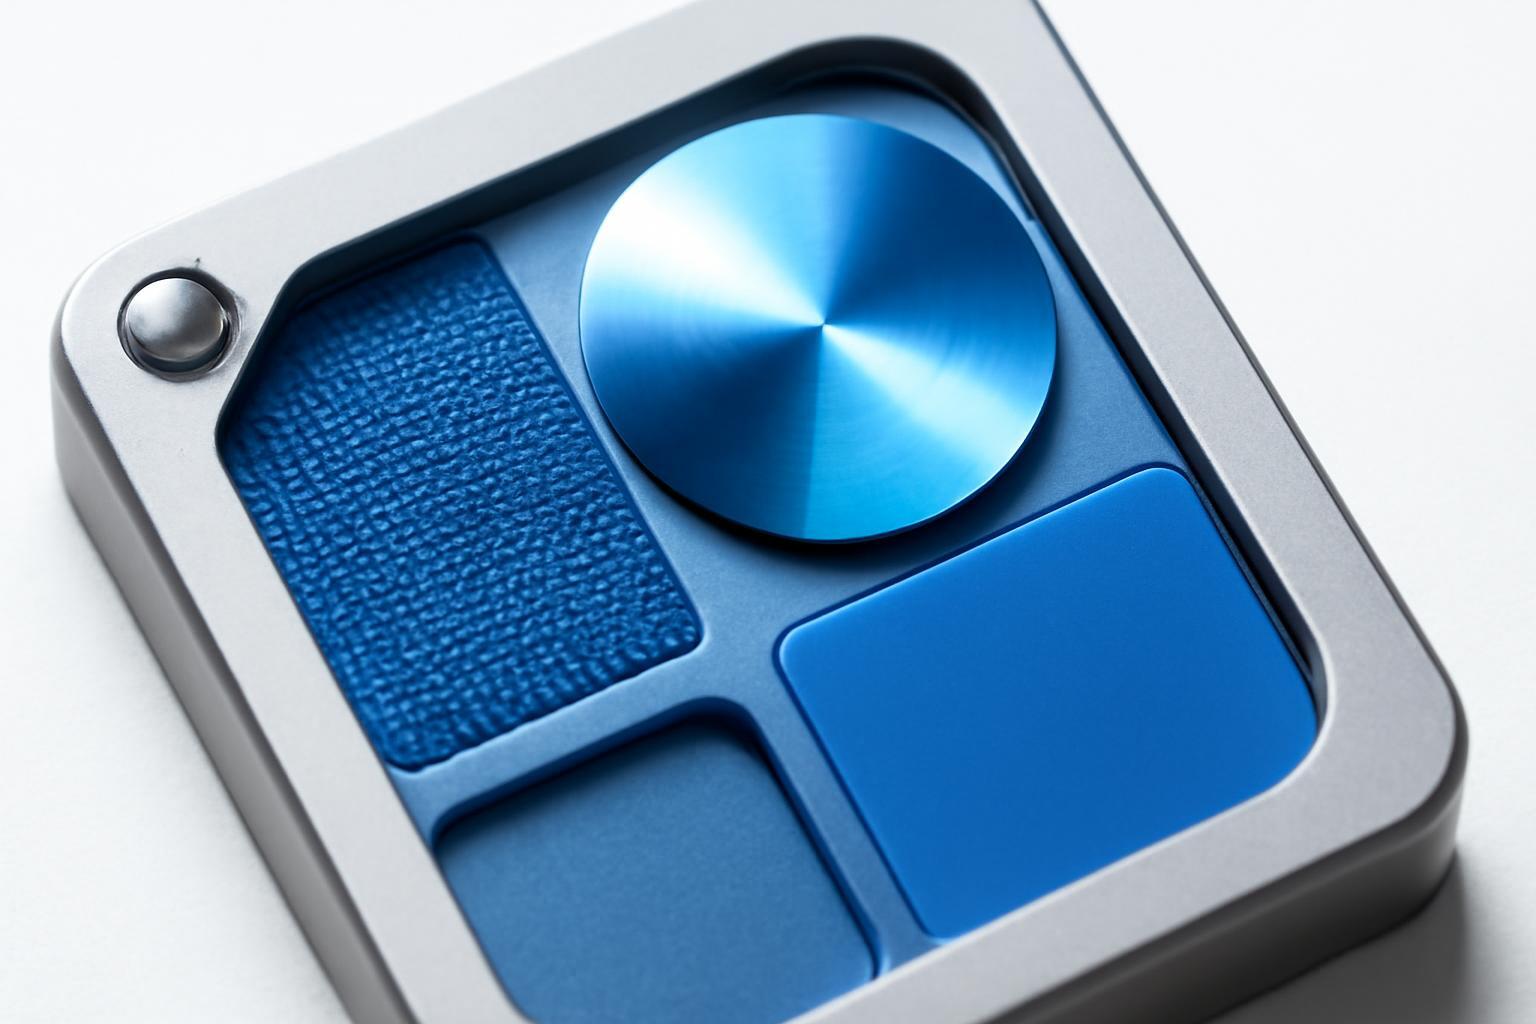
Why one color behaves differently on fabric, metal, and plastic
The eye does not see color as an abstract quantity — it sees light reflected from a surface. And surfaces reflect light completely differently. Metal reflects mirror-like: a ray falls and bounces off almost at the same angle, so the color on metal strongly depends on the viewing angle and especially misbehaves with metalllic reds. Fabric scatters light — cotton or polyester fibers catch the ray and scatter it in all directions, which makes the color look softer and more matte. Plastic can behave any way it wants: from almost mirror gloss to semi-transparency if the material is thin or originally light-permeable.
Let's add texture to this. Glossy surface — lacquered metal, polished plastic — can increase color saturation by 15–25% compared to the standard. Matte, like uncolored cotton or rough plastic, can mute the color by 20–30%. That is, the same RAL code on gloss and matte fabric — visually two different colors, although the paint formula is identical.
Metamerism: when colors match only under one light
Metamerism is a phenomenon where two samples appear identical under one light source but diverge under another. A classic trap: the brand blue on a metal plate and on fabric match under office fluorescent lamps (standard D65, daylight 5000K), but once both samples are taken outdoors or under warm LED 2700K light — the difference becomes obvious.
The reason is that paints and pigments have different spectral composition of reflected light on different materials, even if they appear identical under certain lighting conditions. For a brand this is critical: the sign at the entrance is illuminated by outdoor LED, while the employees' uniforms are lit by daylight from the window. If both samples are not checked under multiple light sources during the approval stage, metameric effects will manifest in the finished advertising campaign.
What metrics to use to avoid arguing 'by eye'
The dispute between the designer and manufacturer about whether the colors are 'similar' is resolved not by taste, but by a number. The main tool is the ΔE (delta E) indicator, which measures the distance between two colors in color space.
| Value of ΔE | What it means | Applicability |
|---|---|---|
| < 1 | The difference is imperceptible to the human eye | Reference for premium brands, packaging of luxury goods |
| 1–3 | Acceptable deviation | Industrial control standard (GOST R 59953—2021) |
| > 3 | Visible deviation | Requires recertification of color with the manufacturer |
Besides ΔE, three levels of color coding are used when working with different materials — and they should not be confused. Pantone and RAL are physical standards tied to a specific pigment and substrate: they indicate what the color is made of. RGB and HEX exist only on screen and are not directly transferable to production. CMYK works for printing on paper and cardboard, but poorly predicts results on fabric sublimation or powder coating of metal. Therefore, in a brandbook each material must have its own reference color code, not one universal HEX for all cases.
Case: RAL 3020 on metal, fabric and plastic
Let us take a specific example — saturated red RAL 3020, popular in the identification of transport and industrial equipment. On powder-coated metal with a glossy finish, this color may appear brighter and "warmer" than the standard by approximately 15–20% due to mirror reflection and glossy texture. On unimpregnated cotton fabric, the same pigment looks muted, slightly darker, and matte — scattered light diminishes its saturation. On unfinished plastic, the behavior is unpredictable: if the material is slightly translucent, the red visually "sinks" into the depth and loses density, whereas on dense glossy plastic it nearly replicates metal.
The practical conclusion from this case: one cannot claim that "red on metal is brighter than on fabric" in isolation from the type of coating. The difference is determined not by the material per se, but by the combination of material + texture + lighting. It is this combination that must be fixed in the brand specification, not relying on a single Pantone code.
Visual harmony instead of scientific accuracy
To require ΔE
In practice, this means: if the brand color is deep blue, then on metal it may shift toward a cooler tone, and on fabric — toward a slightly muted shade, and this is normal if both variants are perceived by the observer as "that same brand blue," rather than as two different colors. The mistake of most brand books is to demand scientific precision where perceptual consistency is needed.
How to prepare a brand book with consideration for different materials
The palette should be developed once, with a view to future production, not adjusted post-factum to fit each new medium. The process is as follows:
- Fix the master color in the Pantone or RAL system as the main brand benchmark — this is the starting point for all calculations.
- For each type of material (fabric, metal, plastic, paper), specify a separate reference code with an acceptable ΔE range, rather than a single HEX value.
- Specify the type of lighting under which conformity is checked — D65 standard is mandatory, and additionally warm LED 2700K for metameric checking.
- Specify adjustments for texture: for glossy finishes, build in a reduction in saturation of the benchmark by 15–20%, for matte finishes — increase by the same 20–30%, so that the final visual result matches.
- Coordinate with the manufacturer the tolerance between batches — within one batch the deviation is almost imperceptible, but between different batches it can be visible, especially on saturated red tones, so it is important to request control samples with each new purchase.
- Check the final result not from the screen file, but from a physical sample under different light sources — the screen will never show metamerism.
Such an approach eliminates endless post-factum revisions: the manufacturer receives not an abstract HEX, but a specific instruction with tolerances for their material, while the brand manager receives a guarantee that the signage, packaging, and uniform will be perceived as a unified system, even if the digital color values on them differ slightly.
Recent articles
MegaFon, BMW, VTB and more 240+ companies. See how it looks in the showcase reel:






Our branding agency is approached to order:
Branding agency services












